The smart Trick of R Vand Technology That Nobody is Discussing
Table of ContentsR Vand Technology Can Be Fun For EveryoneExcitement About R Vand TechnologyThe Definitive Guide for R Vand TechnologyThe Best Guide To R Vand TechnologyThe Best Strategy To Use For R Vand Technology
, various other makers and equipment are additionally set up with the corresponding CNC, which makes the manufacturing market in its support, greatly enhancing the top quality and efficiency. (3D printing) to develop a brand-new manufacturing method - hybrid additive subtractive production (HASM).CNC device Summary Image Equates programs being composed of specific numbers and letters to move the pin (or workpiece) to different areas and depths. Can either be a Vertical Milling Center (VMC) or a Straight Milling Center, depending on the positioning of the pin.
Most CNC mills need positioning the work surface on or in them and must go to the very least as large as the workpiece, yet brand-new 3-axis machines are being generated that are a lot smaller sized. Cuts workpieces while they are rotated. Makes quickly, precision cuts, typically making use of indexable devices and drills. Reliable for challenging programs developed to make components that would be unfeasible to make on manual lathes.
R Vand Technology for Dummies

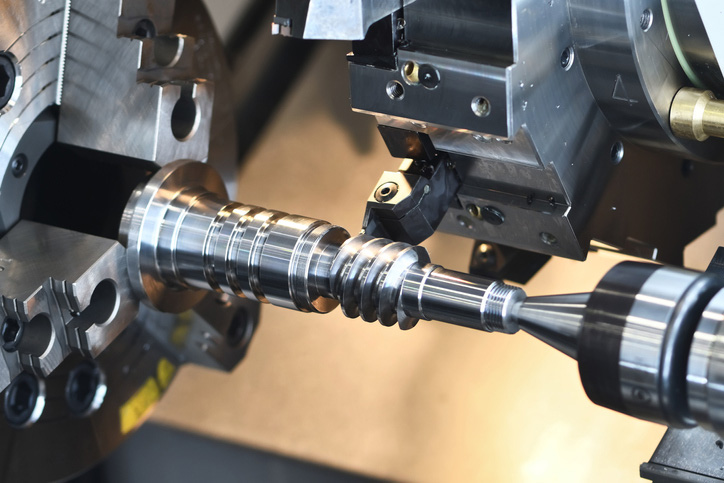
Normally have two axes (X and Z), but more recent designs have more axes, permitting even more innovative work to be machined. Most modern-day lathes have online tooling, permitting limited milling operations to occur without needing to eliminate the part from the turret spindle. Second operations can be completed by using a sub-spindle, which is co-axial to the primary spindle, yet faces the other instructions.
Entails cutting a material making use of a plasma lantern. Frequently utilized to cut steel and other steels, yet can be used on a variety of products. In this procedure, gas (such as compressed air) is blown at high speed out of a nozzle; at the very same time, an electric arc is developed via that gas from the nozzle to the surface area being cut, turning some of that gas to plasma.
EDM can be broadly divided into "weight" type procedures, where the electrode is the positive shape of the resulting function in the part, and the electric discharge deteriorates this attribute right into the component, causing the negative form, and "cord" kind procedures. Weight processes are rather slow as compared to standard machining, averaging like 100 mm3/min, as compared to 8 million mm3/min for traditional machining, yet it can create functions that conventional machining can not.
Everything about R Vand Technology
This is beneficial for complex profiles with inside 90 level edges that would certainly be challenging to device with traditional approaches. Electrolyte service saturates the workpiece, and voltage is applied in between the weight, top, and workpiece, bottom. Considered to be very effective by boosting productivity with automation.
Multi-spindle devices have numerous spindles on a drum that revolves on a straight or upright axis. The drum has a drill head which includes numerous spindles that are placed on ball bearings and driven by gears. There are 2 kinds of accessories for these drill heads, repaired or adjustable, depending on whether the center distance of the drilling spindle requires to be differed.
All about R Vand Technology
Some waterjet cutters have a 5-axis cutting head, permitting for much even more complex forms to be cut, and to compensate for the angle of the kerf to leave the angled wall on the supply as opposed to on the completed part. Waterjet cutting equipment Utilized to quickly punch openings and reduce thin materials.
Punch presses are normally used when a CNC mill would mishandle or unfeasible. https://rvandtechnlgy.bandcamp.com/album/r-vand-technology. CNC strike presses can come in the C framework, where the sheet product is secured onto a machining table and a hydraulic ram presses down on the material, or they can can be found in a portal framework variant where bar stock/tubing is fed right into the machine
A light collision might not damage the device or tools but might damage the component being machined to ensure that it must be ditched. Numerous CNC tools have no integral sense of the outright setting of the table or tools when transformed on. They need to be manually "homed" or "zeroed" to have any kind of referral to work from, and these limitations are simply for figuring out the place of the component to work with it and are no difficult motion limitation on the mechanism.
See This Report on R Vand Technology
Equipments geared up with lots sensors can quit axis or pin motion in action to an overload condition, however this does not protect against a collision from taking place. If the drive system is weak than the equipment's architectural integrity, then the drive system merely presses versus the obstruction, and the drive electric motors "slide in area".